Skip to content

How to Choose the Best Plastic Mold Design in China?

Choosing the best plastic mold design in China requires more than comparing supplier quotations. It requires evidence, technical judgment, and careful communication. PlasticsEurope’s Plastics—The Fast Facts 2024 reports global plastics production of 413.8 million tonnes in 2023. That scale creates intense demand for reliable, repeatable, and efficient molding systems.

China offers broad manufacturing capacity, but supplier quality varies significantly. A factory may show polished samples while hiding weak cooling layouts or limited maintenance support. Look closely. Review steel grades, mold-flow analysis, ejection design, tolerances, and previous production records. Ask for measured cycle times, not optimistic promises. The cheapest quotation may become expensive after repeated flash, warpage, or premature component failure.

John P. Beaumont, a recognized injection molding authority, describes the mold as “the heart of the injection molding process” in his technical work on mold design. His point remains practical: a mold influences part quality, cycle time, tooling life, and production stability. A strong plastic mold design should therefore match the resin, machine, annual volume, surface finish, and expected service life.

The China Plastics Processing Industry Association and international market reports consistently highlight automation, efficiency, and quality control as major manufacturing priorities. However, published market figures do not guarantee one supplier’s performance. Factory audits still matter. So do trial shots.

The right decision is rarely obvious. It often requires challenging the first design. Evaluate technical documents, inspect workmanship, and test the mold under realistic production conditions. This approach reduces avoidable risk and supports a more dependable long-term partnership.
How to Choose the Best Plastic Mold Design in China?

Define Part Requirements: Resin Shrinkage of 0.1%–2.5% and Tight Tolerances

Choosing a plastic mold in China starts with measurable part requirements, not a supplier’s catalog. Resin shrinkage can range from 0.1% to 2.5%, depending on polymer type, filler content, flow direction, and cooling conditions. A 100 mm feature may therefore change by 0.1 to 2.5 mm. That difference can ruin an assembly fit. ISO 294-4:2018 and ASTM D955-08(2020) provide recognized methods for measuring molding shrinkage, but laboratory values are not production guarantees.

Share the resin grade, expected shrinkage range, critical dimensions, and tolerance limits before mold design begins. For a 50 mm housing, a ±0.05 mm tolerance requires stronger process control than a general ±0.20 mm tolerance. Gate location matters. So does wall thickness. A 2 mm wall beside a 4 mm rib may cool unevenly and pull the part out of shape. Mold engineers should review packing pressure, cooling channels, steel allowance, and expected warpage. In practice, I have seen teams specify tight tolerances before testing the actual resin. That is risky.

Use a trial mold or scientific molding study when dimensions are critical. Record cavity pressure, mold temperature, cycle time, and measurements from several shots. Industry guidance consistently favors capability studies over single-part inspection. Still, the first design may be imperfect. Shrinkage data can disagree with real production results. Leave controlled adjustment steel where possible, especially around bores, clips, and sealing surfaces. A precise drawing cannot compensate for uncertain material behavior.

Choose Mold Types for China Production: 100,000–1,000,000+ Shot Lifespan

Choosing the best plastic mold design in China starts with the required shot lifespan. A 100,000-shot mold suits prototypes, seasonal products, and limited market tests. It often uses simpler construction and fewer cavities. A 300,000-shot mold supports stable production with stronger steel, replaceable inserts, and better cooling channels. For products exceeding 1,000,000 shots, the mold needs highly durable materials, precise machining, and carefully protected moving parts.

Shot estimates should match the resin, part geometry, and production cycle. Glass-filled plastic can wear gates and runners faster than standard resin. Thin ribs may require higher injection pressure, increasing stress around the cavity.

During design reviews, ask for cavity count, expected cycle time, steel specifications, and maintenance intervals. A mold producing four parts every 30 seconds has a different workload from a single-cavity tool running every 60 seconds. The numbers matter.

I once underestimated maintenance downtime on a high-volume project. That mistake affected the delivery schedule. A reliable Chinese mold supplier should provide trial-shot records, dimensional reports, and a clear spare-parts plan. Inspect flash, sink marks, ejection marks, and cooling performance during testing.

For one million shots, planned polishing and seal replacement are not optional. They are part of the design. Still, a longer lifespan does not automatically mean better value. An oversized mold can waste money when demand remains uncertain.

Verify DFM Standards: 0.5°–2° Draft Angles and Uniform Wall Thickness

How to Choose the Best Plastic Mold Design in China?

Verify DFM Standards: 0.5°–2° Draft Angles and Uniform Wall Thickness

A reliable plastic mold design begins with a careful DFM review. Draft angles between 0.5° and 2° usually support clean part release. However, textured surfaces, deep cavities, and soft materials may require more draft. A smooth-looking CAD model can still hide ejection problems. I have seen minor sidewall friction cause scratches during mold trials. Engineers should check every vertical surface, not only the main cavity.

Uniform wall thickness also reduces sink marks, warpage, and uneven cooling. Keep nominal walls consistent wherever possible. Sudden thickness changes often create weak or visibly distorted areas. Ribs should usually remain thinner than the main wall, often around 40% to 60% of its thickness. Rounded transitions are safer than sharp internal corners. These details sound basic, but production pressure can make them easy to overlook.

Tips: Request a marked-up DFM report before tooling begins. Confirm draft values with section views, not guesses. Review material shrinkage and texture requirements together. Ask for mold-flow analysis when the geometry is complex. A first review is rarely perfect, so leave room for practical revisions after trial molding. Reliable suppliers should explain risks clearly and record each approved change.

How to Choose the Best Plastic Mold Design in China? - Verify DFM Standards: 0.5°–2° Draft Angles and Uniform Wall Thickness
DFM Design Dimension Recommended Design Target Typical Verification Method Why It Matters for Mold Performance Risk if Ignored Evaluation
Draft Angle 0.5°–2° per side for standard smooth surfaces. Use a larger angle for textured, deep, or high-friction surfaces. Review the 3D model with draft analysis software and confirm the angle relative to the mold-opening direction. Supports clean part ejection, reduces sidewall friction, and helps protect both the molded part and cavity surface. Drag marks, whitening, deformation, sticking, or damage to textured surfaces. Recommended
Uniform Wall Thickness Keep wall sections as consistent as practical. For many injection-molded thermoplastic parts, a general starting range is 1.5–3.0 mm, subject to resin and geometry. Use wall-thickness analysis and compare each section with the selected resin supplier’s processing guidance. Promotes balanced filling, predictable cooling, and more stable shrinkage. Sink marks, voids, warpage, short shots, and uneven dimensional results. Recommended
Wall-Thickness Transition Use gradual transitions and avoid abrupt changes. A gradual taper is generally preferable to a sudden step between thick and thin areas. Inspect section transitions in the CAD model and review flow simulation results where geometry is complex. Reduces localized cooling differences and improves melt-flow consistency. Localized sink, weld lines, air traps, residual stress, or warpage. Recommended
Rib Thickness Keep ribs approximately 40%–60% of the adjoining nominal wall thickness to reduce sink risk. Measure rib-to-wall ratios in the CAD model and check the back surface for visible sink potential. Provides stiffness without creating excessive material buildup behind the rib. Visible sink marks, cosmetic defects, longer cooling time, and warpage. Recommended
Boss Design Use a hollow boss with a controlled wall thickness rather than a solid mass. Add supporting ribs where structural strength is required. Review boss-to-wall spacing, core geometry, and local thickness using 3D section analysis. Improves cooling uniformity and reduces material concentration around fastening features. Sink marks, voids, cracking, poor screw retention, or ejection problems. Recommended
Fillets and Radii Apply internal radii wherever possible. Avoid sharp internal corners, especially where walls, ribs, and bosses intersect. Run CAD radius checks and review stress-sensitive areas with mold-flow or structural analysis when needed. Improves melt flow, reduces stress concentration, and makes machining and polishing easier. Cracking, difficult filling, sharp machining transitions, and premature mold wear. Recommended
Gate Location Place the gate to support balanced filling and direct weld lines away from critical cosmetic or load-bearing areas. Use mold-flow analysis to evaluate fill time, pressure, weld-line position, and packing balance. Influences appearance, weld-line strength, fiber orientation, packing effectiveness, and cycle stability. Flow hesitation, visible gate marks, unbalanced filling, weld-line weakness, or excessive injection pressure. Geometry Dependent
Vent Depth and Venting Provide vents at the end of fill and around inserts or shut-offs. Vent dimensions must be matched to the resin and tool design. Check vent positions in the mold layout and verify burn marks or trapped-air areas during trials. Allows displaced air and gases to escape while limiting flash formation. Burn marks, short shots, weld-line defects, trapped air, and unstable filling. Geometry Dependent
Cooling Layout Locate cooling channels at a consistent distance from the cavity surface and concentrate cooling around thick or slow-cooling areas. Review cooling-channel spacing, circuit balance, and predicted temperature distribution. Controls cycle time, dimensional stability, and warpage. Uneven shrinkage, long cycles, hot spots, and part deformation. Critical
Parting Line Place the parting line on a non-critical or less visible area when possible, while maintaining adequate shut-off surfaces. Inspect the parting-line proposal in the 3D mold layout and check for undercuts and flash-sensitive edges. Determines mold complexity, flash control, cosmetic appearance, and ejection strategy. Visible mismatch, flash, difficult machining, unintended witness lines, or added tooling complexity. Recommended
Undercuts and Side Actions Eliminate unnecessary undercuts. Use lifters, slides, or collapsible mechanisms only when the product function requires them. Run an undercut analysis and confirm the required stroke, clearance, wear surfaces, and ejection sequence. Reduces mold cost, maintenance requirements, and cycle-time risk. Higher tooling cost, complex maintenance, part damage, or mold interference. Use Only When Needed
Ejector Placement Distribute ejectors on structurally strong areas and keep them away from visible or cosmetic surfaces where possible. Review ejection-force distribution and confirm that the part will not distort during release. Promotes balanced ejection and reduces stress or visible ejector marks. Ejector whitening, deformation, sticking, cracks, or uneven release. Recommended
Shrinkage Allowance Use the resin’s published molding-shrinkage range and validate the allowance through trial results rather than applying one universal value. Compare material data, tool steel dimensions, first-article measurements, and process conditions. Improves dimensional accuracy and supports controlled tool correction if required. Out-of-tolerance parts, difficult tool correction, and inconsistent assembly fit. Material Specific
Material Compatibility Select mold steel, surface treatment, gate design, and cooling strategy according to resin abrasiveness, corrosiveness, shrinkage, and processing temperature. Cross-check the resin technical data sheet with the mold-material and process specifications. Improves tool life, surface quality, corrosion resistance, and production consistency. Premature wear, corrosion, poor release, dimensional drift, or surface defects. Material Specific
Note: Draft angle, wall thickness, shrinkage, gate design, venting, and cooling requirements depend on the resin, part geometry, surface texture, tooling material, and production conditions. Final values should be confirmed through a formal DFM review and, where appropriate, mold-flow analysis and first-article inspection.

Optimize Steel and Cooling for 70–140 MPa Injection Pressure

How to Choose the Best Plastic Mold Design in China?

Injection pressure between 70 and 140 MPa demands careful steel and cooling decisions. A mold may look robust, yet thin ribs can still deflect during filling. Choose mold steel according to resin abrasiveness, production volume, and expected maintenance. Hardened steel supports long cycles, while pre-hardened steel may suit moderate production. Check cavity corners, sliders, and ejector areas closely. These zones often reveal stress before the first maintenance review.

Tips: Ask the supplier for steel certificates, hardness records, and cooling-channel drawings. Keep channels close to the cavity, but maintain enough steel for strength. Use balanced circuits when cavity temperatures differ. Measure water flow, not just water temperature. Small details matter.

For pressure near 140 MPa, thicker support plates and stronger locking areas can reduce flash and deformation. Cooling should remove heat evenly around gates, deep cores, and thick sections. Conformal channels can improve temperature control, but conventional drilled channels remain easier to inspect and repair. Select based on measurable results, not impressive drawings.

In practical mold reviews, I have seen cooling layouts approved too quickly. The mold ran, but cycle time stayed high. That decision needed more testing. Ask for filling analysis, pressure estimates, cooling studies, and a documented trial plan. Confirm part weight, dimensions, surface quality, and ejection performance during sampling. A reliable Chinese mold partner should explain compromises clearly, including what may need improvement after the first trial.

Evaluate Chinese Moldmakers Through ISO 9001, Trials, and Inspection Data

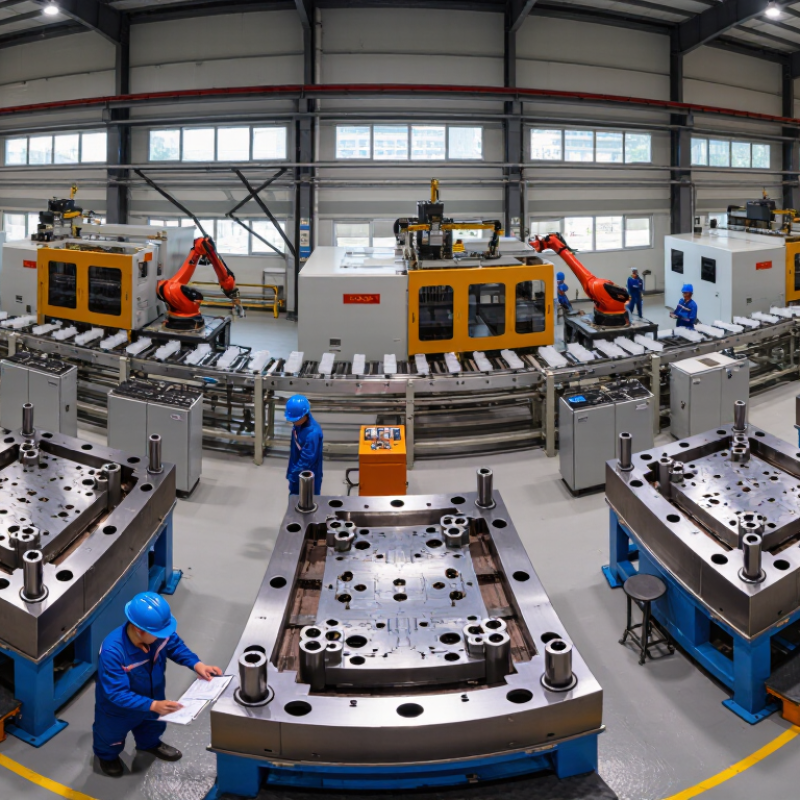
Choosing the best plastic mold design in China requires evidence, not attractive drawings or low quotations. I usually begin by checking the moldmaker’s ISO 9001 system. Ask how they control design changes, supplier materials, machining records, and corrective actions. Certification helps, but it does not guarantee a perfect mold.

Request trial records from similar projects. During a mold trial, observe filling balance, venting, ejection, cycle time, and visible flash. Ask for measured results from several shots, not one approved sample. A reliable team should explain why a gate location, cooling layout, or steel choice suits your resin and production volume. Their answers should match the design data.

Inspection reports reveal more than polished presentations. Review cavity dimensions, wall thickness, warpage, shrinkage, and part weight. Check whether measurements come from calibrated equipment, such as a coordinate measuring machine, and whether sampling points are clearly defined. Photos of the first samples can help, but numbers matter more.

I once trusted a clean report too quickly. The mold later showed uneven cooling near a deep rib. That mistake taught me to compare trial data with real production conditions. A moldmaker may pass an audit and still need stronger process discipline. Leave room for questions. Ask what failed, how it was corrected, and whether the same risk could return during mass production.

Scroll To Top